Top Contract Manufacturing Organizations for Global Buyers

Choosing among the top contract manufacturing organization partners requires more than comparing production prices. Global buyers need evidence, consistency, and a clear understanding of operational risk.

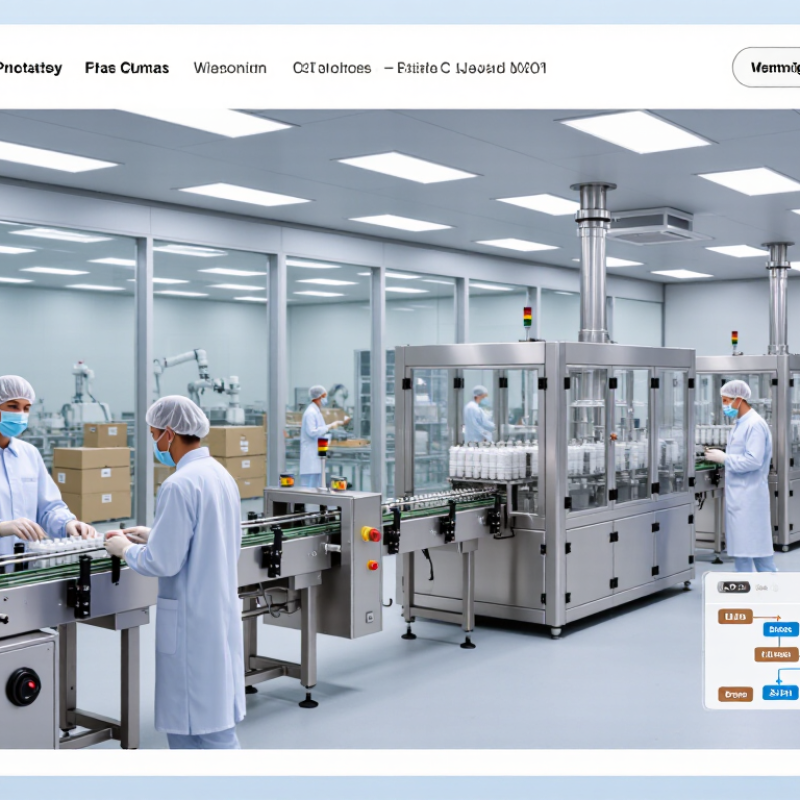
A capable partner can support development, commercial production, packaging, and reliable supply planning. Yet capabilities listed on a website prove very little. Buyers should examine inspection histories, quality agreements, batch-release procedures, and technology-transfer experience. They should also review how the site manages deviations, supplier changes, data integrity, and temperature-controlled shipments. A clean facility matters. So does disciplined communication.

Jim Miller, founder of PharmSource and a longtime pharmaceutical outsourcing analyst, has stated, “Contract manufacturing is not simply a capacity solution; it is a strategic decision about risk, quality, and control.” His observation remains practical for buyers evaluating international suppliers. The strongest partnerships usually include defined escalation paths, measurable service levels, and transparent cost assumptions. They also respect regional requirements without treating compliance as paperwork alone.

Details reveal maturity. Ask who owns process knowledge. Ask how quickly a failed stability result reaches the customer. Ask what happens when demand rises suddenly. The answers may be uncomfortable. That is useful.

No contract manufacturing organization is perfect, and every selection involves trade-offs. A large network may offer resilience but feel less flexible. A specialized facility may provide deeper expertise but fewer backup options. Buyers should test these weaknesses before signing, not after a shipment is delayed. Trusted partners earn confidence through documented performance, technical openness, and steady quality over time.

Top Contract Manufacturing Organizations for Global Buyers

Definition and Role of Contract Manufacturing Organizations

Contract Manufacturing Organizations (CMOs) produce goods for other companies under a formal manufacturing agreement. They may handle formulation, raw materials, processing, packaging, testing, or documentation. Their role is more than factory capacity. A capable CMO turns approved specifications into repeatable production. It also helps buyers manage quality, timelines, and supply continuity across markets.

For global buyers, a CMO should provide transparent records and measurable controls. These include batch instructions, equipment maintenance logs, deviation reports, and release testing. Site visits can reveal practical details that documents miss, such as material flow, operator training, and storage conditions. A strong partner communicates early when a process changes. Silence creates expensive surprises. However, a polished facility does not guarantee perfect performance. Buyers still need independent checks, clear acceptance criteria, and regular performance reviews.

Tips: Define responsibilities before signing. Specify quality standards, change-control procedures, delivery terms, and audit rights. Ask how the CMO handles rejected materials and unexpected delays. Review sample records, not only presentation slides. Small gaps matter. Keep technical instructions current, because outdated documents can weaken an otherwise reliable process. Use staged production when possible, especially before approving larger volumes. This approach may feel slower, but it exposes process weaknesses while correction remains practical.

Key Services Offered by Global Contract Manufacturers

Top Contract Manufacturing Organizations for Global Buyers

Global contract manufacturers now support more than production. They provide formulation development, process optimization, analytical testing, scale-up, packaging, and supply-chain coordination. Grand View Research estimated the global contract manufacturing market at over USD 240 billion in 2023. This growth reflects stronger demand for flexible capacity and specialized technical skills.

Quality systems remain central. Experienced manufacturers usually operate controlled facilities, validated processes, electronic batch records, and documented deviation management. They may also support stability studies, method transfer, regulatory documentation, and cold-chain logistics. The 2024 Global Outsourcing Survey from Deloitte found that organizations increasingly assess providers through resilience, technology, and measurable business value, not price alone. That is important. A cheaper quote can hide expensive delays.

Global buyers should examine real operating evidence. Ask for audit histories, release timelines, complaint rates, capacity plans, and change-control procedures. Process development teams should explain how laboratory results become repeatable commercial batches. Packaging services need equal attention, especially for temperature-sensitive or moisture-sensitive products. The World Health Organization has repeatedly identified supply-chain quality and traceability as critical healthcare priorities. Yet no manufacturer is perfect. Even strong facilities can face raw-material shortages, equipment failures, or unclear communication. A detailed quality agreement, transparent escalation route, and frequent technical reviews reduce these risks. Small gaps matter.

Standards for Evaluating International Manufacturing Partners

International manufacturing partners should be judged by evidence, not polished presentations. Factory capability matters, but consistent performance matters more. Review quality records, inspection results, process controls, and corrective action reports from recent production. Ask how the facility handles defects, delayed materials, and sudden design changes. Clear answers reveal operational maturity.

A credible partner can provide current certifications, traceability records, worker safety procedures, and environmental compliance documents. Verify them independently when possible. Visit the production site or arrange a live remote audit. Look closely at calibration labels, storage conditions, line cleanliness, and rejected parts. Small details often expose larger weaknesses. Records matter.

Communication deserves equal attention. Define technical specifications, acceptance criteria, packaging rules, delivery milestones, and escalation contacts in writing. Confirm intellectual property safeguards and data access controls before sharing sensitive files. Request customer references from comparable markets, then ask about missed deadlines and recovery actions. No partner is flawless. I once underestimated response speed because the sample quality looked excellent. That mistake delayed later decisions. A controlled pilot order, measurable service levels, and regular performance reviews create stronger evidence than promises alone.

Top Contract Manufacturing Organizations for Global Buyers

Standards for Evaluating International Manufacturing Partners

This buyer-side benchmark allocates 100 evaluation points across internationally recognized priorities, including GMP quality systems, regulatory readiness, supply-chain resilience, technical transfer capability, and commercial transparency. The model is designed for comparing manufacturing partners without using company or brand-specific performance data.

Leading Regions and Capabilities in Contract Manufacturing

Global contract manufacturing is shifting from low-cost sourcing toward regional resilience and specialized capabilities. The 2024 Global Life Sciences Outlook reports continued investment in biologics, cell therapies, and sterile production. These areas require validated cleanrooms, cold-chain control, and experienced quality teams. A buyer may need more than available capacity.

North America remains strong in clinical manufacturing, regulatory expertise, and complex biologics. Europe offers mature pharmaceutical engineering, advanced packaging, and strong quality systems. Asia-Pacific continues to expand in active ingredients, medical devices, electronics, and large-scale production. The International Federation of Pharmaceutical Manufacturers and Associations notes that pharmaceutical research and development spending remains heavily concentrated in North America and Europe, while manufacturing capacity is growing across Asia.

Market estimates vary. Fortune Business Insights values the global contract development and manufacturing market at tens of billions of dollars, with biologics among its fastest-growing segments. The numbers are useful, but imperfect. Definitions differ between reports. A practical assessment should examine inspection history, batch-release timelines, technology-transfer records, and backup utilities. Visit the site if possible. Look for labeled material flows, temperature logs, and clean maintenance records. Regional proximity helps, but capability depth matters more. A nearby facility without analytical testing can create expensive delays. A distant partner with strong process validation may prove safer, though transport risks remain.

Top Contract Manufacturing Organizations for Global Buyers - Leading Regions and Capabilities in Contract Manufacturing

Leading Region Commonly Outsourced Manufacturing Capabilities Typical Product Formats Regulatory and Quality Environment Key Buyer Advantages Important Buyer Considerations
United States and Canada Commercial-scale small-molecule manufacturing, biologics, sterile processing, clinical supply, cell and gene therapy, analytical testing, and specialized drug-device assembly. Tablets, capsules, liquids, prefilled systems, vials, lyophilized products, recombinant proteins, vaccines, and advanced therapies. Strong alignment with United States and Canadian good manufacturing practice requirements; extensive inspection, validation, data-integrity, and supply-chain expectations. High technical depth, mature clinical-to-commercial transfer, strong intellectual-property controls, and access to advanced development services. Often higher operating costs; capacity for sterile, biologic, and advanced-therapy programs may require early reservation.
Western and Northern Europe Small molecules, biologics, vaccines, sterile fill-finish, highly potent compounds, oral solid dosage, clinical packaging, and complex formulation development. Tablets, capsules, injectables, biologic drug substance, prefilled syringes, inhalation products, and temperature-sensitive medicines. Established European Union good manufacturing practice framework with strong Qualified Person oversight, batch-release controls, and pharmacovigilance expectations. Strong regulatory credibility, mature quality systems, advanced process science, and efficient access to European clinical and commercial markets. Energy, labor, and compliance costs can be significant; cross-border supply planning must account for serialization and regional release requirements.
Central and Eastern Europe Generic medicines, oral solid dosage, semi-solids, sterile products, packaging, analytical testing, and selected active pharmaceutical ingredient operations. Tablets, capsules, creams, ointments, liquids, ampoules, vials, and secondary-packaging formats. Operations commonly serve European Union requirements and may be subject to national authority inspections and centralized market controls. Competitive manufacturing economics, established pharmaceutical workforce, and geographic proximity to major European distribution networks. Capability depth varies by site; buyers should verify inspection history, technical-transfer experience, and capacity for highly complex products.
India Active pharmaceutical ingredients, generic medicines, oral solid dosage, specialty formulations, biosimilars, sterile products, and clinical-trial supplies. Tablets, capsules, dry powders, injectables, ophthalmic products, inhalation products, and biologic drug substance. Facilities may operate under Indian good manufacturing practice requirements as well as United States, European, or other importing-market standards. Broad formulation expertise, large pharmaceutical talent pool, strong generic-drug infrastructure, and generally competitive production costs. Due diligence should include site-specific inspection records, data-integrity controls, raw-material traceability, and export-market compliance history.
China Active pharmaceutical ingredients, intermediates, small molecules, biologics, vaccine-related manufacturing, sterile products, and process-development services. Chemical intermediates, APIs, tablets, capsules, vials, prefilled formats, recombinant products, and selected advanced therapies. Facilities may be approved for domestic and international markets; requirements differ according to the destination market and product category. Large industrial base, extensive chemistry capability, strong scale-up resources, and broad supplier ecosystems for materials and equipment. Buyers should assess geopolitical exposure, export controls, intellectual-property protections, business continuity, and supply-chain concentration.
Japan and South Korea High-quality small molecules, biologics, vaccines, sterile injectables, cell and gene therapy support, advanced drug delivery, and precision analytical services. Injectables, biologics, vaccines, oral solids, transdermal systems, specialized delivery devices, and temperature-controlled products. Sophisticated national regulatory systems with strong quality expectations and increasing alignment with international technical standards. Excellent process control, automation, advanced biotechnology expertise, and strong manufacturing consistency. Capacity can be selective; qualification timelines, language requirements, and higher technical service costs should be included in project planning.
Singapore and Southeast Asia Biologics, vaccines, sterile fill-finish, oral solid dosage, medical nutrition, active ingredients, packaging, and regional supply-chain services. Biologic drug substance, vials, syringes, tablets, capsules, liquids, and temperature-controlled products. Singapore has a highly developed regulatory and quality environment; requirements across other Southeast Asian markets vary by jurisdiction. Strategic access to Asian markets, strong logistics infrastructure, growing biotechnology capabilities, and attractive regional manufacturing networks. Buyers should evaluate country-specific registrations, import controls, temperature-management requirements, and differences in local regulatory maturity.
Latin America Generic medicines, branded-generic formulations, oral solid dosage, liquids, semi-solids, sterile products, packaging, and regional market supply. Tablets, capsules, syrups, creams, ointments, injectables, and consumer-health formats. National regulatory requirements apply, with standards and approval timelines differing across individual markets. Regional market knowledge, shorter distribution routes for local demand, and potential advantages for Spanish- or Portuguese-language packaging. Market-by-market registration, currency, customs, infrastructure, and demand-forecast risks require careful local planning.
Buyer evaluation dimensions: manufacturing technology, dosage-form experience, regulatory inspection history, quality-system maturity, technical-transfer capability, available capacity, supply-chain resilience, data integrity, intellectual-property protection, sustainability practices, and total delivered cost. Regional capability descriptions are general market-level observations; qualification should always be completed at the individual manufacturing-site level.

Selection Process for Global Buyers

Selecting a contract manufacturing organization requires more than comparing hourly rates. Global buyers should examine quality systems, technical capability, capacity, and communication practices. A polished presentation can still hide weak controls.

Request recent audit summaries, validation records, deviation procedures, and batch-release examples. Confirm whether the facility follows recognized quality standards and supports the regulations in each target market.

Review its experience with your product type, equipment, packaging needs, and scale-up plans.

A site visit can reveal practical details, such as material flow, storage conditions, and operator training. Ask how quickly the team reports problems. Delays create expensive surprises.

My own early evaluations sometimes overvalued modern equipment. That was a mistake. Reliable documentation and disciplined change control often matter more than impressive machinery.

Buyers should also test supply continuity by checking secondary suppliers, inventory policies, and shipping routes.

Pricing deserves careful review. The lowest quotation may exclude testing, technical transfers, tooling, or quality investigations.

Tips:

Build a weighted scorecard before discussions. Include quality, compliance, capacity, risk, service, and total cost. Interview the quality lead, not only the sales team. Request clear answers in writing. Start with a limited technical project when practical, then assess communication, timelines, and corrective actions. Leave room for doubt. Some risks appear only after production begins.